How To Calculate The Upper Specification Limit
A specification for the width of a component for example might be 27 mm - 002 mm. Parameter that will assure all CQAs will be within limits without out of specification OOS events.
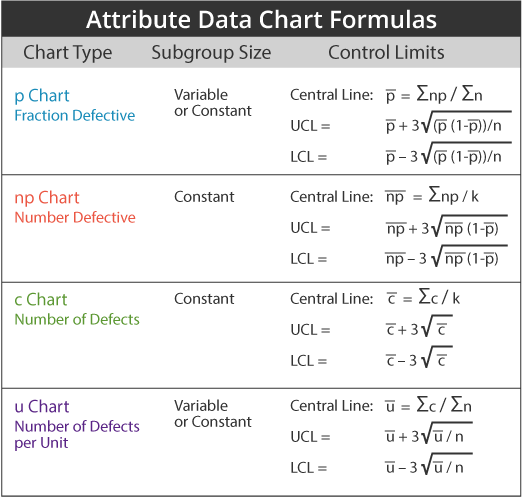
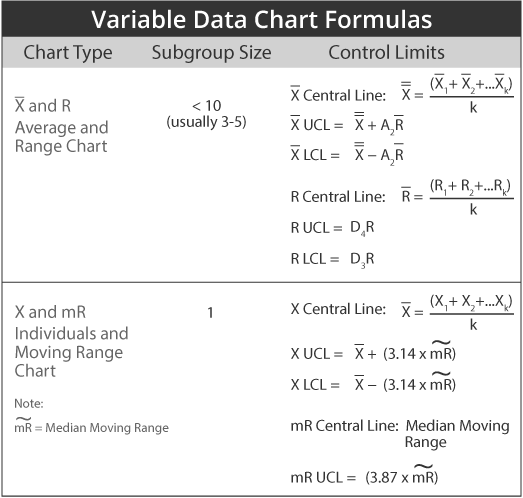
Statistical Process Control Spc Tutorial
Z upper 3316 from above C pk 3316 3 110.
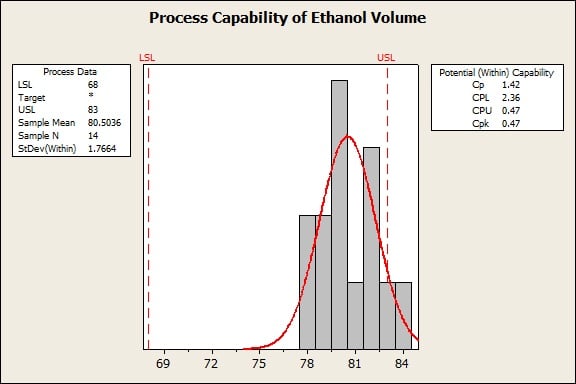
How to calculate the upper specification limit. This works and I have used it several times. Z values are used to determine the percentage of output that is outside the specification limits using the standard normal distribution table. Since we are trying to measure how many standard deviations fit between the center line and the specification limit you should not be surprised that the value of those limits the process mean and the standard deviation are all components of the Z.
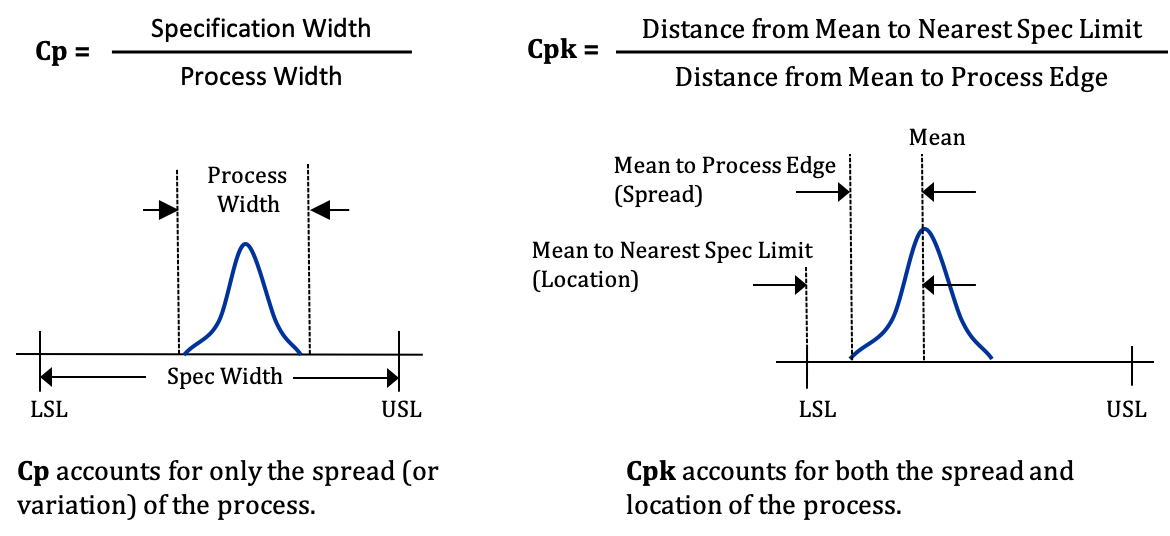
Engineering specifications 60 5. How do you calculate upper and lower limits. A negative Cpk indicates the mean fell outside of the specification limits SL.
The formula for sigma depends on the type of data you have. Formulas for calculating control chart upper and lower control limits. Is well within the specification limits then the difference between the Upper specification U and Lower specification L should be larger than 6σ 4 p c 6 S UpperSpec LowerSpec P 6 S UpperSpec LowerSpec P p.
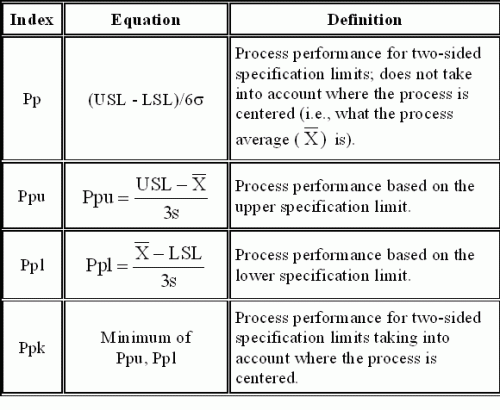
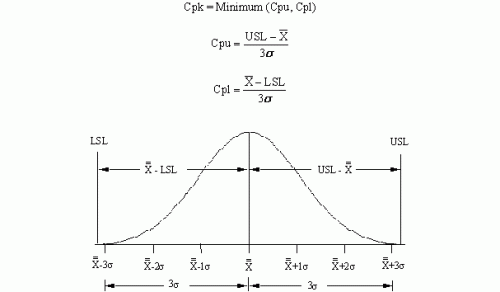
To find Cpk you need to calculate a Z score for the upper specification limit called Z USL and a Z score for the lower specification limit called Z LSL. If the customer has no expectations for the function performance or quantity of the product then I would suggest that you make the lower specification limit zero and the upper specification limit infinity that way you will be assured that your process capability for weight will always be greater than 133. A Misleading C pk.
The lower specification limit LSL represents the target fall of your process. Be notified via email. USL 65 LSL 55.
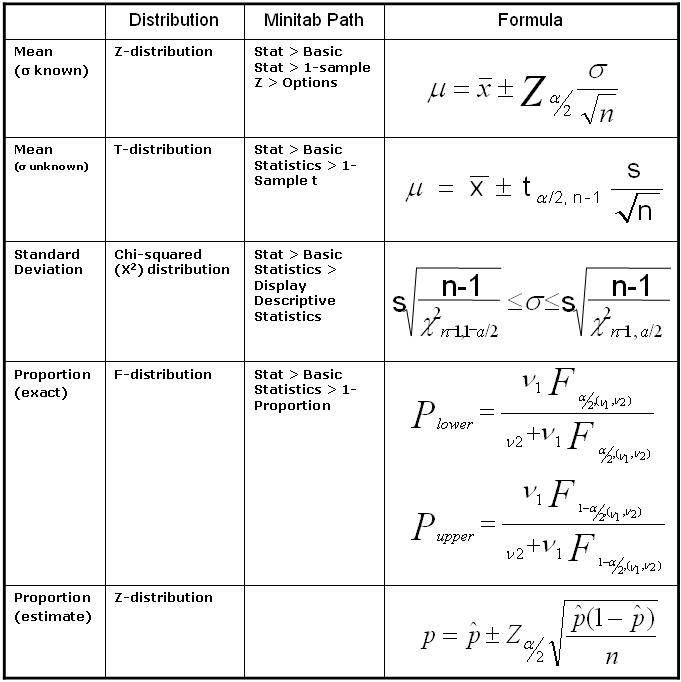
Calculate confidence interval of the mean. Z min becomes Z upper and C pk becomes Z upper 3. USL Upper Specification Limit 49C LSL Lower Specification Limit 39C Standard Deviation 2C Mean 40 To Find Process Capability Process Capability Index.
The Z value that is used in calculating process capability is the distance of the process average from the specification limits measured in standard deviation units. Subtract three times the standard deviation from the average to get the lower control limit. Next determine the mean of the data.
Next determine the standard deviation. Minitab calculates a one-sided process variation by dividing the study variation statistic by 2. The first step in determining the percent outside the USL is to calculate the Z value for the upper specification.
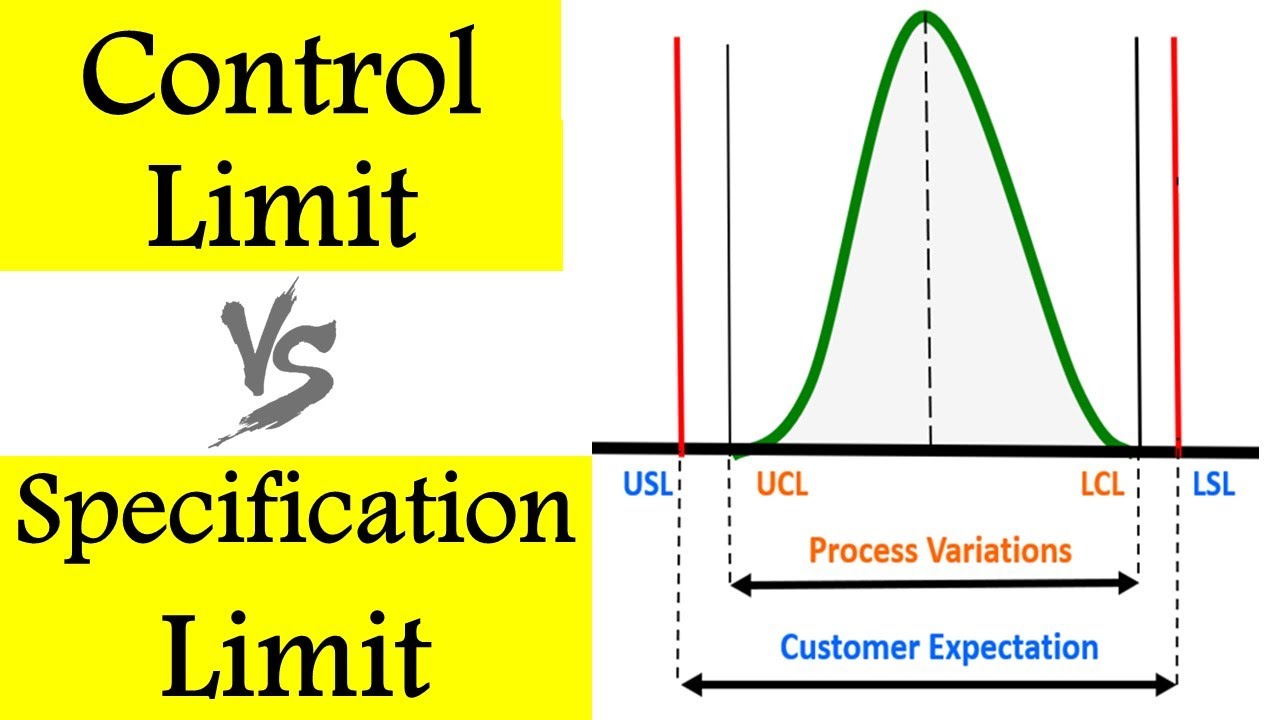
These are the upper and lower limits of the specifications. A tolerance is the distance from the upper specification limit to the lower specification limit. As the example demonstrates setting the lower specification to 0 results in a lower misleading C pk.
Estimate where the two lines should be located in reference to the overall average and the tails of the curve. The upper specification limit USL represents the target rise of your process. 3 sigma Upper Control Limit UCL - 3 sigma Lower Control Limit LCL Why are there so many formulas for sigma.
A C pk of 110 is more realistic than one of 0005 for the data given in this example and is more representative of the process itself. Upper Specification Limit USL c 6 s LSL Where c Process Capability Index s Process Standard Deviation Example. The lower specification is 2500 inches and the upper specification is 2687 inches.
Upper and Lower Limit Calculation with Capability Formula. Calculate the engineering Tolerance. Engineering tolerance is 65 55 10.
In the example the lower specification limit LSL is 0 minutes on time and the upper specification limit USL is 14 minutes. LSL 25 USL 2687. For unilateral tolerance calculate.
These are simply 1 sigma 2 sigma and 3 sigma from the center line. Find the average and standard deviation of the sample. This is will be the average of all data points.
Absolute value in case SPEC. In the example of 28 mm - 002 mm the USL 2802 mm. Find the upper specification limit of a process whose index is 500 process standard deviation is 25 and the lower specification limit LSL is 100.
It is found by subtracting the grand average from the USL and dividing by the standard deviation. Tolerance design is the focus of this paper and discussion. For these cases Minitab uses the following method.
Process capability 6 6s 6 x 23232 139392. First determine the upper and lower limits. Find the percentage below the lower specification 53.
How does Minitab calculate tolerance when I enter a one-sided tolerance. The lower specification limit is 55 but no upper specification limit exists. Examples of upper and lower specification limits.
Any labels that are smaller than 25 inches or larger than 2687 inches are unacceptable. Calculate the percent of output outside the USL. Find the percentage above the upper specification 52.
Draw vertical lines on the distribution to represent the lower and upper specification limits. Then set the upper spec tolerance at plus 4 sigma from the upper confidence limit and the lower tolerence spec at minus four sigma from the lower confidence limit. Draw the specification limits on the distribution.
When a tolerance is defined there is a clear target. Add three times the standard deviation to the average to get the upper control limit.
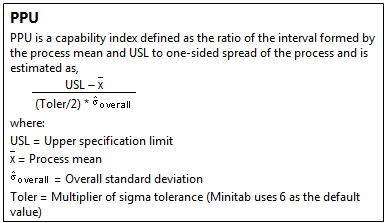
How Cpk And Ppk Are Calculated Part 1

Spc Software Statistical Process Control Improve Your Bottom Line Infinityqs
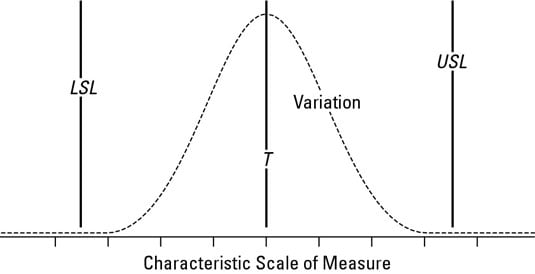
How To Define Six Sigma Specifications Dummies
Process Capability Statistics Cp And Cpk Working Together

Sybeq What Process Variation Component Do Cp Cpk Capture

Process Capability Analysis With Python By Roberto Salazar Geek Culture Medium
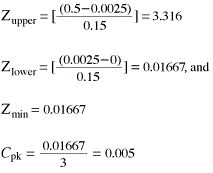
Calculate Capability Indices With Only One Specification
Process Capability Part 3 Bpi Consulting
Control Limit Vs Specification Limit Difference Between Control Limits And Specification Limits Youtube
A Guide To Process Capability Cp Cpk And Process Performance Pp Ppk 1factory

Upper Specification Limit Usl Definition
Statistical Process Control Spc Tutorial
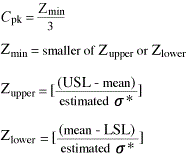
Calculate Capability Indices With Only One Specification
Difference Between Control Limits And Specification Limits


2 Ways To Calculate Six Sigma For Continuous And Discrete Data Sixsigmastats
Confidence Interval Ci
Process Capability Part 2 Bpi Consulting
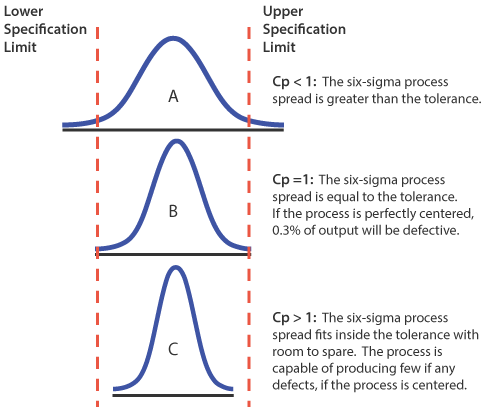
Statistical Process Control Spc Tutorial

Control Limits And Specification Limits Sap Documentation

Posting Komentar untuk "How To Calculate The Upper Specification Limit"